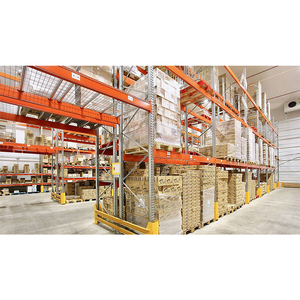
Powder Coated Steel OEM Custom Size Heavy Duty Selective Pallet Rack
- Bay Capacity:Up to 15,000 kg
- Steel Grade:Q235B / Q355B
- Pitch Adjustability:50mm / 75mm

No matching pages. Try "pallet", "mezzanine" or "cantilever".
Explore our heavy-duty industrial storage systems, manufactured from certified Q235B and Q355B prime high-tensile steel. Each system is engineered to withstand precise dynamic load distributions, seismic loads, and rigorous logistics throughput.
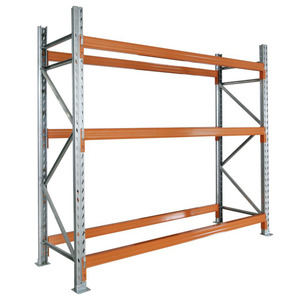
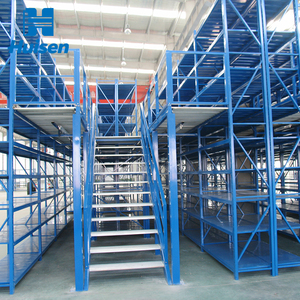
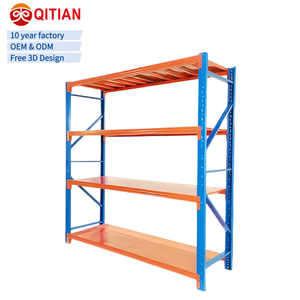
In modern industrial logistics, warehouse floor space commands premium capital expenditure. Very Narrow Aisle (VNA) racking systems represent the apex of selective high-density pallet storage by reducing aisle dimensions down from the conventional 3.2m–3.8m to a tightly controlled 1.5m–1.9m corridor. By combining vertical elevation extensions of up to 18 meters with 100% direct pallet selectivity, VNA configurations deliver a 40% to 55% volumetric storage gain across identical warehouse footprints.
Structural Integrity Mandate: Operating at aisle tolerances under 200mm between MHE chassis and steel uprights requires strict compliance with EN 15512 static calculation standards and EN 15620 Class 100/200/300 floor deflection criteria. Every millimeter of frame plumbness directly prevents costly mast collision incidents.
Engineered from continuous roll-formed Q355B micro-alloyed coil steel. The multi-bend Omega geometry provides superior torsional stiffness and high moment of inertia ($I_x, I_y$), effectively counteracting lateral buckling under extreme concentrated vertical loads up to 28,000 kg per bay.
Boxed profile beams are fitted with heavy-duty robotic welded end connectors featuring 5 cold-stamped claws. This creates a moment-resistant semi-rigid joint with high rotational stiffness ($C_d$), drastically minimizing frame drift and beam sag under deflection limits of $L/200$.
Dual-mode alignment infrastructure: High-strength continuous ground guide rails (100×50×5mm cold-formed angle or structural channel) anchored with dynamic expansion fasteners, or embedded inductive electromagnetic wire frequencies operating at 5–10 kHz for seamless turret truck steering.
A primary failure mode in non-certified VNA installations is the disregard for concrete floor flatness and slab deflection. Because high-reach VNA trucks (Man-Up or Man-Down turret trucks) operate with masts exceeding 15 meters, the smallest irregularity in the concrete floor slab is magnified exponentially at the top beam level. Under European standard DIN 18202 and VDMA 15251, VNA systems mandate Superflat floor finishes conforming to Class F-min 100 or EN 15620 Class 300 tolerances.
Our engineering export department produces full site FEA (Finite Element Analysis) stress simulations prior to manufacturing. We calculate combined live loads, dead weights, seismic acceleration coefficients ($S_a$), wind shear in open-sided facilities, and mechanical impact allowances (accidental impact loads of 2.5 kN across aisles according to EN 15512). Reinforced baseplates, dual floor anchoring using Grade 8.8 chemical or wedge anchor bolts, and floor-level column wrap-around guards are specified as mandatory structural components.
| Storage System Type | Aisle Width (mm) | Max Usable Height | Pallet Selectivity | Floor Utilization | Handling Equipment | Relative Capex |
|---|---|---|---|---|---|---|
| VNA Pallet Racks (CE Certified) | 1,500 – 1,850 mm | Up to 18.0 m | 100% Direct | Up to 65% | VNA Turret / AGV / Stacker | Optimized Moderate |
| Standard Selective Racks | 3,200 – 3,800 mm | Up to 11.5 m | 100% Direct | 35% – 40% | Counterbalance / Reach Truck | Baseline Low |
| Double Deep Pallet Racking | 2,900 – 3,300 mm | Up to 11.0 m | 50% Direct (LIFO) | 45% – 50% | Double-Deep Reach Truck | Low-Medium |
| Drive-In / Drive-Through | Lane Dependent | Up to 10.0 m | Poor (LIFO/FIFO) | 60% – 70% | Standard Counterbalance | Moderate |
| Automated ASRS Cranes | 1,400 – 1,600 mm | Up to 35.0 m | 100% Direct | 75% – 85% | Automated Stacker Crane | Very High |
Global supply chains are transitioning toward automated intralogistics, sustainability certifications, and micro-fulfillment centers. Sourcing managers and industrial logistics developers must align rack procurement with these five paradigm shifts.
Autonomous Mobile Robots (AMRs) and automated VNA turret trucks are displacing manual reach forklifts. Buyers require cold-rolled racks with optical navigation reflectors, laser-cut fiducial target slots, and ultra-tight upright plumb tolerances (1:1000) for robotic gripper pick precision.
As urban industrial land costs surge across North America, Europe, and the Middle East, vertical storage heights are climbing from 10m to 16m–18m. Racking procurement now prioritizes spliced heavy-gauge uprights with high moment-resisting splice plates and continuous floor-to-roof engineering.
Global procurement policies mandate Environmental Product Declarations (EPD). Modern exporters must demonstrate electric arc furnace (EAF) low-emission steel sourcing, closed-loop zero-VOC electrostatic powder coatings, and end-of-life 100% material recyclability to satisfy ESG audits.
Procurement specifications increasingly mandate smart sensors embedded within baseplates and lower upright sections. Fiber-optic and MEMS wireless strain gauges detect real-time beam overloading, micro-buckling, and seismic displacement, notifying WMS platforms prior to catastrophic failure.
E-commerce omnichannel distribution hubs demand high-speed piece picking within pallet reserves. Racking procurement contracts now specify hybrid VNA structures combining top-bay pallet reserves with mid-tier integrated catwalks, safety mesh screens, and carton gravity chutes.
As a premier CE-certified pallet rack manufacturer and global exporter, we supply comprehensive, turnkey warehouse storage systems engineered from raw coil to finished seaworthy container delivery.
Every beam, upright column, and row spacer is designed, manufactured, and test-loaded in compliance with EN 15512, EN 15620, and EN 15635 standards, bearing authenticated CE declarations of performance.
Our continuous automated roll-forming lines feature multi-axis computerized precision roll tooling with zero pitch drift across 18-meter single-piece columns, guaranteeing exact beam claw locking without binding.
We provide full structural static calculation sheets, stamped AutoCAD floor plans, and 3D Revit BIM models. Heavy structural steel bundles are steel-strapped with waterproof PE wrapping and air-bag container bracing.
Expert engineering answers to critical inquiries regarding floor slabs, wire guidance systems, forklift compatibility, certification authenticity, and international container shipments.
VNA systems operating with turret trucks above 6 meters require high-precision concrete slabs conforming to DIN 18202 Table 3 Line 4 or VDMA 15251 / EN 15620 (Class 100, 200, or 300). For lift heights exceeding 10 meters, floor flatness must reach F-min 100 or better. If the existing floor fails to meet these criteria, joint grinding or self-leveling epoxy screed pathways must be applied along the truck wheel tracks to prevent mast sway, frame collision, and premature MHE wheel wear.
Mechanical Guide Rails (typically 100×50×5mm or 120×80×6mm steel angles) are physically anchored along the base of the upright frames. They physically constrain the guide rollers of the turret truck, offering zero electronic failure risk and protecting upright bases from forklift collisions. However, they reduce clear floor access for ground pallet placement.
Inductive Wire Guidance utilizes a copper wire embedded 15–20mm below the concrete surface emitting a low-frequency electromagnetic signal (typically 5 kHz to 10 kHz). Wire guidance allows seamless low-level picking, easy housekeeping, and eliminates physical tripping hazards, but requires specialized truck sensors and backup mechanical entrance horns.
True CE certification for industrial racking systems must be supported by an authentic Factory Production Control (FPC) audit under EN 1090-1 (Execution of Steel Structures) and static design calculations executed per EN 15512:2020. Buyers should request: (1) The manufacturer’s CE Declaration of Performance (DoP), (2) Mill test certificates (MTC per EN 10204 3.1) proving yield and tensile properties of Q235B/Q355B coils, and (3) Independent laboratory destructive shear and moment load test reports for beam connectors and upright stubs.
The clear aisle width (Ast) is dictated by the specific material handling equipment model. The calculation formula is: Ast = Overall Truck Width + Pallet Projection + Minimum Safety Clearances. In mechanical rail-guided systems, the nominal clear clearance between guide rails is the truck width over guide rollers plus 100mm (50mm clearance on each side). Clear aisle width between pallet loads is typically 1,600mm to 1,900mm for Euro pallets (1200×800mm) and 1,750mm to 2,050mm for standard industrial pallets (1200×1000mm).
Standard fabrication lead times for 5 to 20 full container loads (40ft HQ) average 20 to 30 calendar days following engineering CAD sign-off and structural review. Custom powder coating colors (RAL spec) or special hot-dip galvanizing for cold storage facilities require approximately 5 to 7 additional days. Ocean transit to European, Middle Eastern, and North American main ports ranges from 18 to 35 days depending on freight routing.
In seismic risk areas (evaluated according to Eurocode 8 or IBC/ASCE 7), standard friction-based upright baseplates are insufficient. We engineer expanded ductile baseplates anchored with heavy chemical anchor arrays, increase column steel wall thicknesses from 2.0mm to 2.5mm or 3.0mm, and install vertical and horizontal spine cross-bracing towers. Dynamic modal response spectrum analysis ensures the rack absorbs oscillatory ground acceleration without structural unseating of pallets.
Provide your warehouse dimensions, clear ceiling heights, pallet specifications, and forklift models. Our licensed structural engineering team will deliver a comprehensive 2D CAD layout, volumetric capacity calculation, and FOB/CIF export pricing within 24 hours.