Maximum Floor Utilization
Eliminates intermediary access aisles required by conventional selective racking. Operating with only one loading and one retrieval aisle converts up to 60-70% more floor space into active cube storage.

No matching pages. Try "pallet", "mezzanine" or "cantilever".
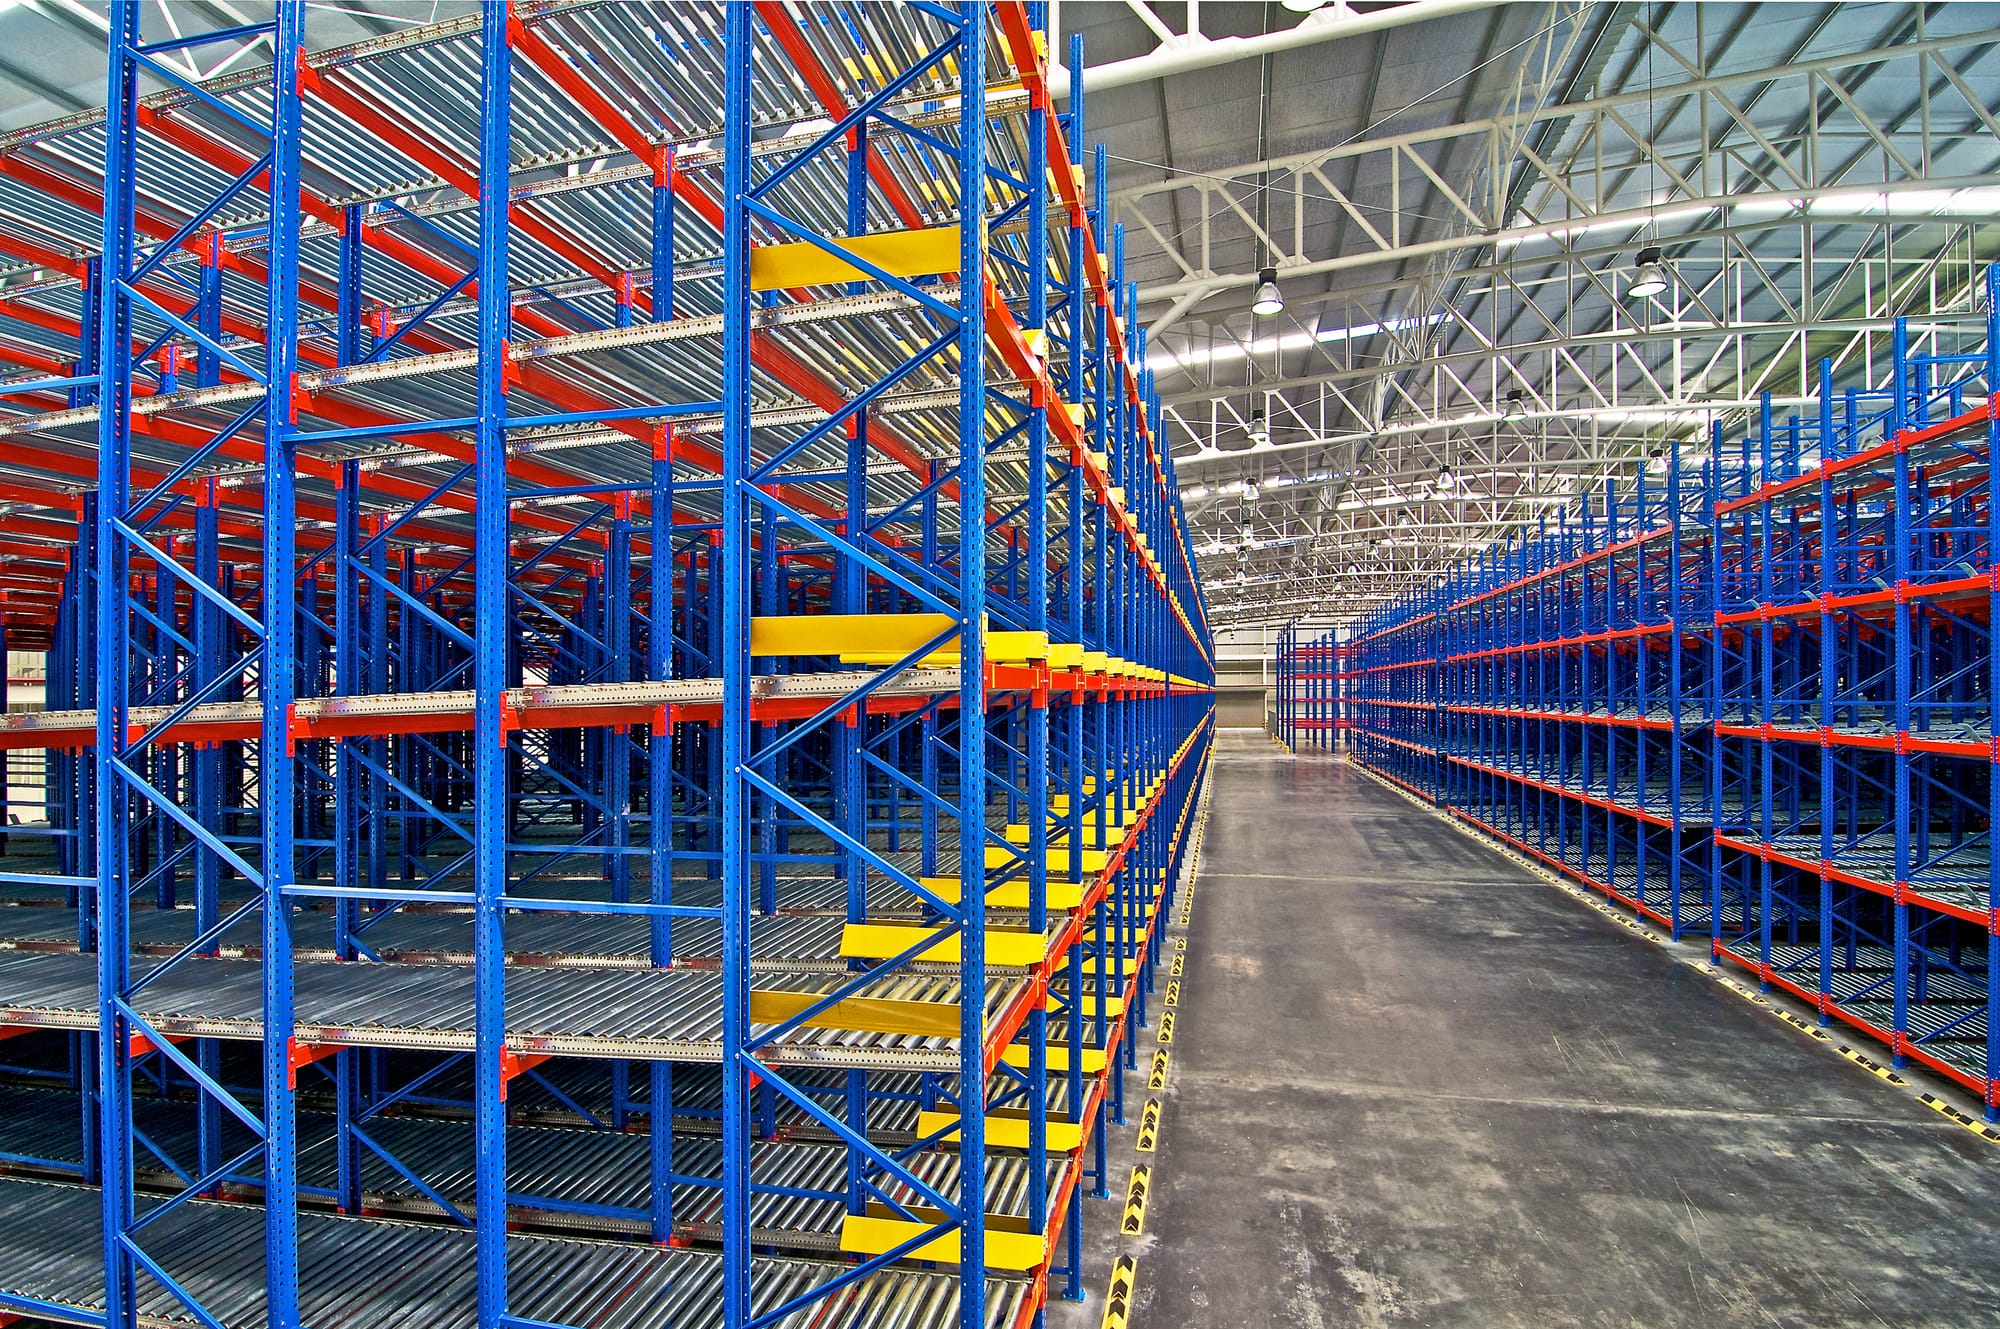
Gravity Pallet Racking, also recognized as Pallet Flow Racking, is a compact dynamic storage solution that leverages gravitational incline to feed pallet loads automatically along heavy-duty roller beds from the replenishment face to the order-retrieval face.
By segregating loading operations from picking aisles, pallet flow racking cuts forklift travel distances by up to 40% and completely prevents vehicle congestion. Each flow lane acts as an autonomous First-In, First-Out (FIFO) conduit, ensuring that date-sensitive goods, pharmaceuticals, and fast-moving food and beverage inventories stay strictly on schedule without risk of obsolete stock.
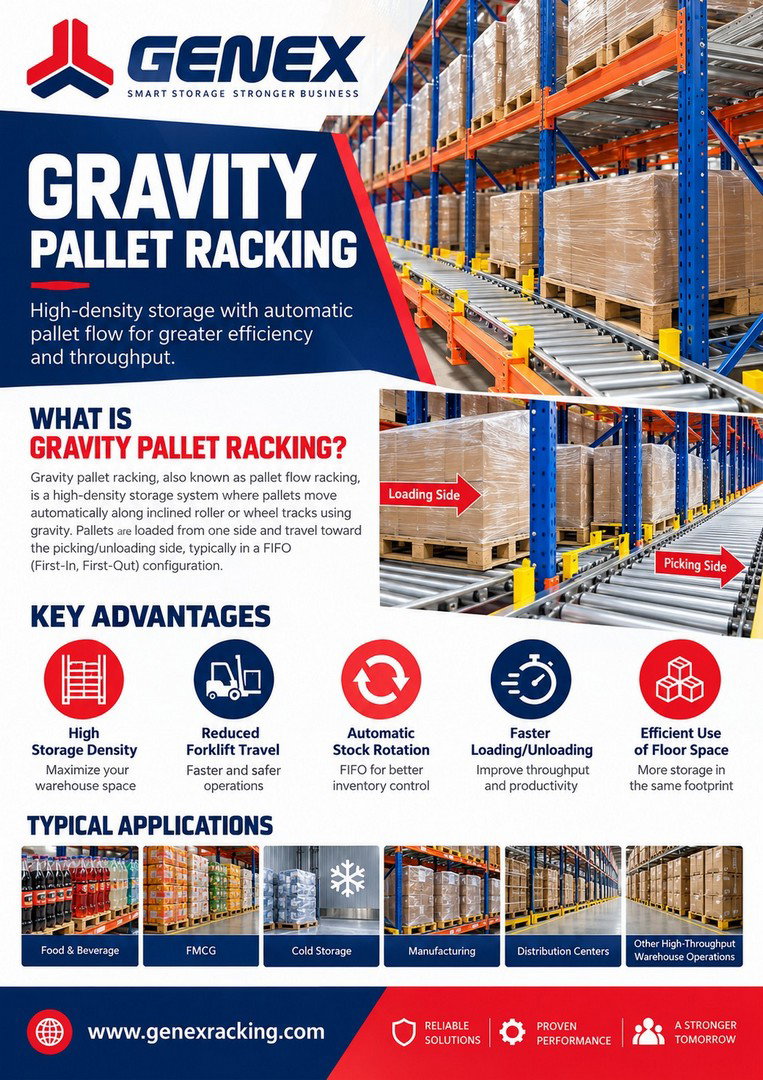
Engineered for high-throughput distribution environments where turnaround speed, space efficiency, and cargo protection are non-negotiable.
Eliminates intermediary access aisles required by conventional selective racking. Operating with only one loading and one retrieval aisle converts up to 60-70% more floor space into active cube storage.
Forklift transit distances are cut significantly because trucks operate solely at dedicated aisle ends. Reduced machine wear, lower battery or fuel consumption, and eliminated cross-traffic bottlenecks increase operational safety.
Physical gravity flow guarantees that the first goods loaded are invariably the first goods unloaded. Ideal for perishable food lines, dairy processing, pharmaceuticals, cosmetics, and seasonal production runs.
Our engineered end separators isolate the leading discharge pallet from trailing pallets. The forklift operator safely extracts the front unit without experiencing hazardous back-pressure from the rear queue.
Because refrigerated and frozen air space carries high energy costs per cubic meter, gravity racking condenses thermal volume, resulting in substantial ongoing utility and cooling efficiency savings.
Integrated magnetic and mechanical brake rollers maintain pallet glide velocities at a constant 0.2 to 0.3 m/s irrespective of lane length or payload weights up to 1,500 kg per pallet.
Every gravity flow system is tailored by GENEX according to pallet quality, unit load dimensions, ambient temperatures, and forklift mast capabilities in compliance with European standards EN 15512 and EN 15620.
| Parameter | Standard Specification | Engineering Notes |
|---|---|---|
| Storage Principle | Strict FIFO (First-In, First-Out) | Separate dedicated replenishment and extraction aisles |
| Track Incline (Gradient) | 3.0% to 4.0% (approx. 1.7° – 2.3°) | Calculated dynamically based on test pallet runner conditions |
| Unit Pallet Capacity | 300 kg to 1,500 kg per pallet position | Custom heavy-duty tracks available for payloads over 1,800 kg |
| Lane Depths Available | 2 to 25 pallets deep | Deep lanes feature intermediate speed controllers every 2-3 positions |
| Speed Braking System | Centrifugal / magnetic internal brake rollers | Maintains continuous travel speed below 0.35 m/s |
| End Separation Mechanism | Automatic mechanical foot / lever separator | Disengages rear line pressure when unloading front pallet |
| Compatible Pallets | Euro (1200x800mm), ISO/GMA (1200x1000mm) | 3-runner wooden or ribbed composite plastic pallets in good condition |
| Operating Temperature Range | -30°C to +45°C | Specially formulated low-temp lubricants & stainless roller hardware |
| Structural Standards | EN 15512, EN 15620, EN 15635 | Hot-rolled / high-tensile cold-formed steel uprights and heavy beam tiers |
Deploying live gravity storage across UAE, GCC, and global supply chains where throughput speed and density are critical.
Maximizes volumetric efficiency in high-cost refrigerated rooms down to -30°C. Minimizing heated corridor volume yields substantial energy savings while maintaining uninterrupted cold-chain FIFO compliance.
Ideal for perishable produce and consumer packaged foods with strict expiration windows. Stock rotation occurs automatically on roller lines without labor-intensive manual date auditing.
Provides strict batch tracking and validation control. Quarantined or tested batch releases glide through lanes in exact manufacturing sequence without the risk of mixed lots.
Gravity pallet racking operates on an engineered incline (usually 3% to 4%) equipped with steel roller conveyors. When a forklift places a pallet into the charge end, gravity glides it smoothly down toward the discharge pick face. Calibrated brake rollers regulate travel speed at safe levels, and a mechanical load separator holds back subsequent pallets until the leading unit is completely picked.
Because loading is confined to the replenishment rear aisle and retrieval is confined to the front discharge aisle, pallets exit in the exact sequential order they were introduced. This First-In, First-Out dynamic prevents product aging, expiration losses, and unnecessary forklift maneuvering.
Pallets must have sound, unbroken bottom deck boards oriented parallel to the roller tracks. High-quality wooden Euro (1200x800mm) or standard industrial (1200x1000mm) pallets as well as reinforced perimeter-base plastic pallets work cleanly. Broken runners, missing nails, or excessive sagging will stop pallet progression and must be rejected before loading.
Yes. GENEX configures specialized cold-storage packages featuring synthetic low-temperature lubricants, galvanized roller tubes, anti-corrosive sealed bearings, and thermal contraction compensation engineered to run reliably down to -30°C.
Because gravity supplies the kinetic movement, there are no electric motors or complex electronic sensors. Scheduled maintenance centers around visual inspections of roller spin, verification of centrifugal brake resistance, clearing stray wood chips from tracks, and testing the trip mechanism of the pallet separator.