Panama Logistics & Free Zone Engineering

CE Certified Drive-In Racking Systems Manufacturers & Exporters serving the Panama market

High-density structural pallet storage engineered to EN 15512 and RMI standards. Turnkey logistics solutions engineered for Colón Free Trade Zone, Panamá Pacífico, and cold chain distribution hubs across Central America.

Export-Grade Heavy Industry Solutions

Engineered Industrial Storage & Pallet Support Systems

Precision-formed cold-rolled structural racks, heavy-duty mezzanine floors, and load-rated components designed for high-density warehouse throughput.

85%
Cubic Volume Utilization
EN 15512
European Structural Standard
4,500+ kg
Bay Load Capacity Tested
ISO 9001
CE Factory Certified Process
High-Density Structural Engineering

Architected for Maximum Volumetric Efficiency in the Panama Canal Corridor

As the primary multimodal hub connecting the Atlantic and Pacific oceans, the Republic of Panama demands extraordinary structural resilience and square-meter productivity from warehouse infrastructure. Real estate adjacent to Puerto de Balboa, Puerto de Manzanillo, and the Colón Free Trade Zone (Zona Libre de Colón - ZLC) operates at high commercial density. Traditional selective pallet racking, while offering universal SKU accessibility, leaves up to 60% of vertical warehouse space unutilized due to extensive aisle-to-storage footprints.

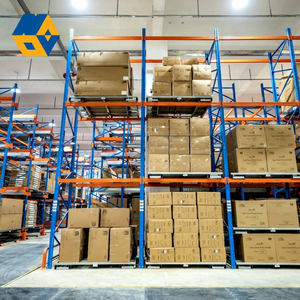
Our CE Certified Drive-In and Drive-Through Racking Systems solve this geometric bottleneck. By eliminating dedicated handling corridors and allowing counterbalance and reach trucks to navigate directly into continuous storage lanes, Drive-In systems elevate warehouse storage capacity by up to 85% compared to conventional static installations.

"Engineered to withstand tropical atmospheric humidity and seismic parameters (REP-2014) in Panama, our drive-in profiles integrate cold-rolled high-tensile Q235B and Q355B structural steel, coupled with automated continuous seam welding for zero deflection under static and dynamic loading."

Every rail bracket, upright column, and cantilever arm is fabricated under stringent factory production controls conforming to European Standard EN 15512 and CE marking directives, ensuring overseas purchasers receive load-tested, turnkey equipment certified for international customs and municipal approvals.

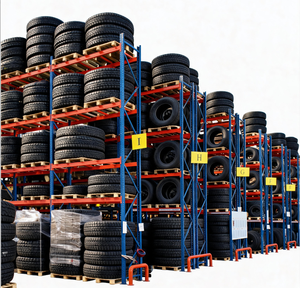
Engineering Parameter Drive-In Racking Selective Pallet Rack
Volumetric Efficiency Up to 85% Cubic Utility 40% – 50% Cubic Utility
Floor Footprint Allocation ~80% Racking / ~20% Aisle ~35% Racking / ~65% Aisle
Pallet Retrieval Model LIFO (FILO) or FIFO (Drive-Thru) 100% Immediate Direct Access
Ideal Pallet SKU Profile Low SKU Variety / Massive Volume High SKU Variance / Small Batches
Cold Storage Operating ROI Maximum (Reduces thermal loss) Moderate (High refrigerated air loss)
Safety & Guide Mechanisms Floor Guidance Rails & Post Guards Aisle End Guarding Only
Strategic Regional Deployment

Panama Industrial Use-Cases & Regional Deployment Scenarios

From bonded free trade operations to pharmaceutical cold chains, our certified drive-in and heavy structural solutions are engineered to address the specific logistics demands of the Isthmus.

Colón Free Trade Zone (ZLC) Bonded Distribution

High-turnover consumer electronics, footwear, apparel, and hardware re-export facilities require immense static buffering within constrained footprints. Drive-in systems allow operators to stage full container loads (FCL) of homogeneous SKUs awaiting transshipment to the Caribbean, Colombia, and Central American ports without wasting vertical floor capacity.

Panamá Pacífico & Tocumen Commercial Logistics Parks

High-throughput regional distribution centers (3PL) located near Tocumen International Airport take advantage of drive-through configurations to create dedicated replenishment faces for inbound air cargo and dispatch lines for regional e-commerce, maximizing throughput per cubic meter while maintaining strict FIFO stock rotation protocols.

Chilled & Frozen Cold Storage Facilities

Refrigeration costs in tropical climates represent a major overhead for import-export logistics. Drive-in racking concentrates pallets densely in -18°C to -25°C cold stores, drastically reducing refrigerated air volume loss. Its dense footprint decreases refrigeration energy expenditure per stored pallet by up to 35%.

Pharmaceutical & FMCG Fast-Rotation Hubs

Panama's regulatory regime requires batch control and climate-controlled storage for pharmaceuticals and healthcare products. Our drive-in channels incorporate specialized load-rail stop blocks, heavy-gauge entrance guide rails, and zinc-plated corrosion-resistant components designed for frequent washdowns and strict sanitized warehouse audits.

Beverage Bottling, Dairy & Bulk Raw Materials

Brewery, carbonated beverage, and dairy manufacturing facilities in Panama City and Chiriquí store high volumes of identical packaging materials and fast-moving end products. Drive-in channels support pallet weights exceeding 1,200 kg to 1,500 kg per position across four to six tiers without structural sway.

Multi-Tier Mezzanine & Industrial Storage Overbuilds

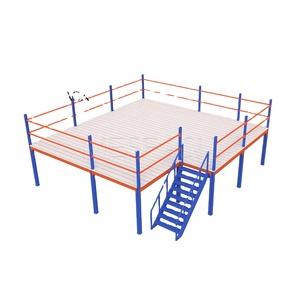
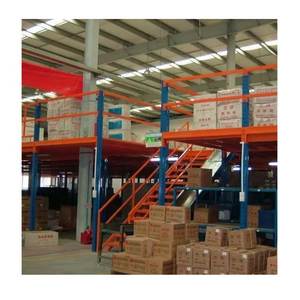
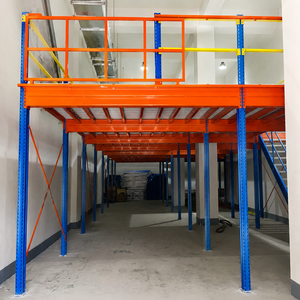
For high-ceiling operations requiring both bulk pallet storage and manual picking levels, our structural mezzanine frames integrate directly above or adjacent to drive-in layouts, doubling working square footage for customs relabeling, repackaging, and SKU consolidation within existing building envelopes.

Market Evolution & Trends

Panama Warehousing Trends: Modernizing Supply Chain Infrastructure

Three converging market dynamics are driving upgrades across Panamanian logistics facilities, requiring enhanced engineering rigor from international racking exporters.

1. REP-2014 Structural & Seismic Design Compliance

Panama sits on complex tectonic fault junctions between the Caribbean, Nazca, and South American plates. Modern warehousing permits enforced by the Ministry of Public Works (MOP) and the Panamanian Society of Engineers and Architects (SPIA) adhere strictly to the Reglamento Estructural de Panamá (REP-2014). Drive-in racks lack interior cross-bracing within drive lanes; therefore, our engineering designs employ heavy-duty top tie beams, portal bracing frames, and heavy-gauge baseplate anchorage to safely absorb horizontal shear forces.

2. Anti-Corrosion Defense Against Tropical Marine Air

With coastal logistics facilities exposed to humid trade winds (relative humidity exceeding 85% year-round) and maritime salt spray from Pacific and Atlantic approaches, surface coatings are critical. We treat upright frames and pallet rails with a high-adhesion electrostatic thermosetting epoxy-polyester powder coat baked at 200°C, supplemented by hot-dip galvanization options for base components, eliminating surface oxidation and rust bleed.

3. Automation Integration: Semi-Automated Radio Shuttle Retrofits

Panamanian distribution centers are modernizing handling workflows by retrofitting conventional drive-in rails into high-throughput semi-automated pallet shuttle channels. Our rack geometries are manufactured with precision roll-formed guide rails that accommodate both standard forklift entry and self-propelled electric radio shuttles, ensuring operations can automate in phases as volume demands scale.

Certified Manufacturing Excellence

Direct Manufacturing Backed by Certified Global Engineering Standards

As a specialized manufacturer and global exporter of heavy-duty warehouse racking solutions, we control the entire structural lifecycle from coil slitting to precision roll-forming, automated robotic welding, multi-stage pre-treatment, and international container stuffing.

Our manufacturing facilities operate under comprehensive ISO 9001:2015 quality assurance frameworks. Every racking component exported to Panama carries CE certification verifying compliance with European Harmonized Standards:

  • EN 15512: Structural design of adjustable pallet racking systems.
  • EN 15620: Tolerances, deformations, and operational handling clearances.
  • EN 15635: Application and user maintenance of storage equipment.
  • RMI (MH16.1): Specification for the design, testing, and utilization of industrial steel storage racks.

We supply clients in Panama with verified 3D CAD layouts, finite element stress analysis reports (FEA), concrete anchor calculations, and full bill-of-materials (BOM) documentation, ensuring smooth municipal sign-offs and trouble-free project handovers.

Our Export & Delivery Commitments to Panama

Ocean Freight Packaging & Stowage Upright frames and beams are nested with heavy corrugated interleaving, edge steel corner protectors, and moisture-barrier shrink wrapping to prevent container transit abrasions and salt moisture condensation.
Turnkey CIF / DDP Delivery Options Seamless logistics delivery straight to Colón Free Zone, Balboa, or directly to your project job site in Panama City, including all export commercial invoices, packing lists, and Certificates of Origin.
Structural Installation Support We provide bilingual step-by-step CAD assembly schematics, video guidance, anchor torque specifications, and can deploy senior installation supervisors directly to Panama for complex multi-tier projects.
Clear Procurement Guidance

Frequently Asked Questions: Purchasing Racking Systems for Panama

Key technical, regulatory, and logistics answers for operations directors, warehouse managers, and supply chain procurement heads in Panama.

1. Why should a logistics operator in Panama choose Drive-In racking over standard selective racking?
Industrial land and warehouse rental prices in strategic locations such as the Colón Free Trade Zone (ZLC), Panamá Pacífico, and Costa del Este are at a premium. Selective pallet racking requires dedicated 3.0m to 3.8m handling aisles between every back-to-back rack row, consuming up to 60% of floor space. Drive-In racking eliminates operating aisles, allowing lift trucks to drive into continuous lanes up to 10 or more pallets deep. This yields up to an 85% increase in total pallet storage capacity, making it the most cost-effective solution for large-batch, low-SKU inventory and temperature-controlled cold stores where cooling empty aisle space is economically inefficient.
2. How do your drive-in racks comply with Panama’s REP-2014 seismic building codes?
Under Panama's Reglamento Estructural de Panamá (REP-2014), industrial pallet racks are classified as building-like structural storage systems requiring verification of horizontal seismic acceleration forces. Because Drive-In systems omit standard diagonal back-bracing within the operational forklift drive lanes, lateral stability must be achieved through rigid top horizontal portal ties, rear spine bracing assemblies, and oversized anchor baseplates anchored with certified M12-M16 chemical or mechanical wedge anchors. Our structural engineers model each installation according to EN 15512 and localized peak ground acceleration coefficients to guarantee system integrity during seismic events.
3. Can your drive-in pallet rails accommodate standard GMA and Euro pallets commonly used in Central America?
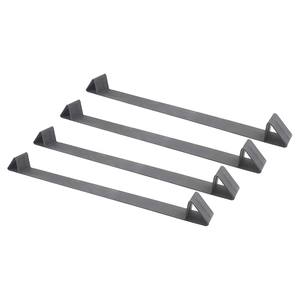
Yes. Warehouses in Panama routinely handle a mix of 1000mm x 1200mm (common North American GMA / Central American standard) and 800mm x 1200mm (European EN 13698-1) pallets, along with plastic containers for cold storage. Our pallet guide rails and cantilever brackets are custom-punched with CNC accuracy to provide optimal load support flanges (typically 65mm to 80mm resting lip width) and incorporate entry flared horns to guide forklift entry smoothly without snagging wooden or plastic pallet overhangs.
4. What protective measures are implemented against forklift impacts inside narrow drive-in channels?
Because forklifts physically operate inside the rack footprint, driver error can impact structural upright columns. To safeguard the installation, we engineer heavy-duty continuous floor-mounted guide rails (structural angle or formed channel) that center the forklift as it enters the bay. Furthermore, we equip outer entrance uprights with 10mm-thick reinforced wraparound steel column protectors, heavy-duty bullnose anchors, and vibrant safety-yellow (RAL 1023) powder coat finishes to prevent impact damage and preserve structural integrity.
5. What is the typical ocean shipping and delivery lead time to the Port of Balboa or Port of Manzanillo?
Standard production manufacturing turnaround for custom drive-in and heavy structural racking projects is approximately 20 to 25 business days following final drawing sign-off. Direct container transit to Panama (discharging at Port of Balboa on the Pacific or Manzanillo / Cristobal on the Atlantic side) typically takes between 24 and 32 days depending on the shipping line schedule. We handle comprehensive export packaging, loading optimization to ensure maximum container space usage (minimizing freight cost per pallet location), and provide all documentation required for rapid customs clearance.
6. What initial warehouse and handling data is required to generate a customized layout and formal quotation?
To generate an optimized CAD proposal and load calculation, our technical team requires: (1) An architectural layout or CAD file of your building showing column grids and clear ceiling heights below sprinklers, (2) Pallet dimensions (W x D x H) including goods overhang and gross pallet weight, (3) Forklift model details (chassis width, overall mast width, collapsed height, and maximum lifting fork height), (4) Temperature profile (ambient dry warehouse, chilled, or -25°C deep freeze), and (5) Operational preference between Drive-In (LIFO) or Drive-Through (FIFO) inventory workflow.

Accelerate Your Panama Logistics Storage ROI

Consult with our structural design team today. We provide full warehouse CAD layouts, seismic load calculations, and competitive factory-direct pricing for projects across the Republic of Panama.

Get Catalog